Foundry Scrap Tracking in ERP: Measure Scrap and Rework
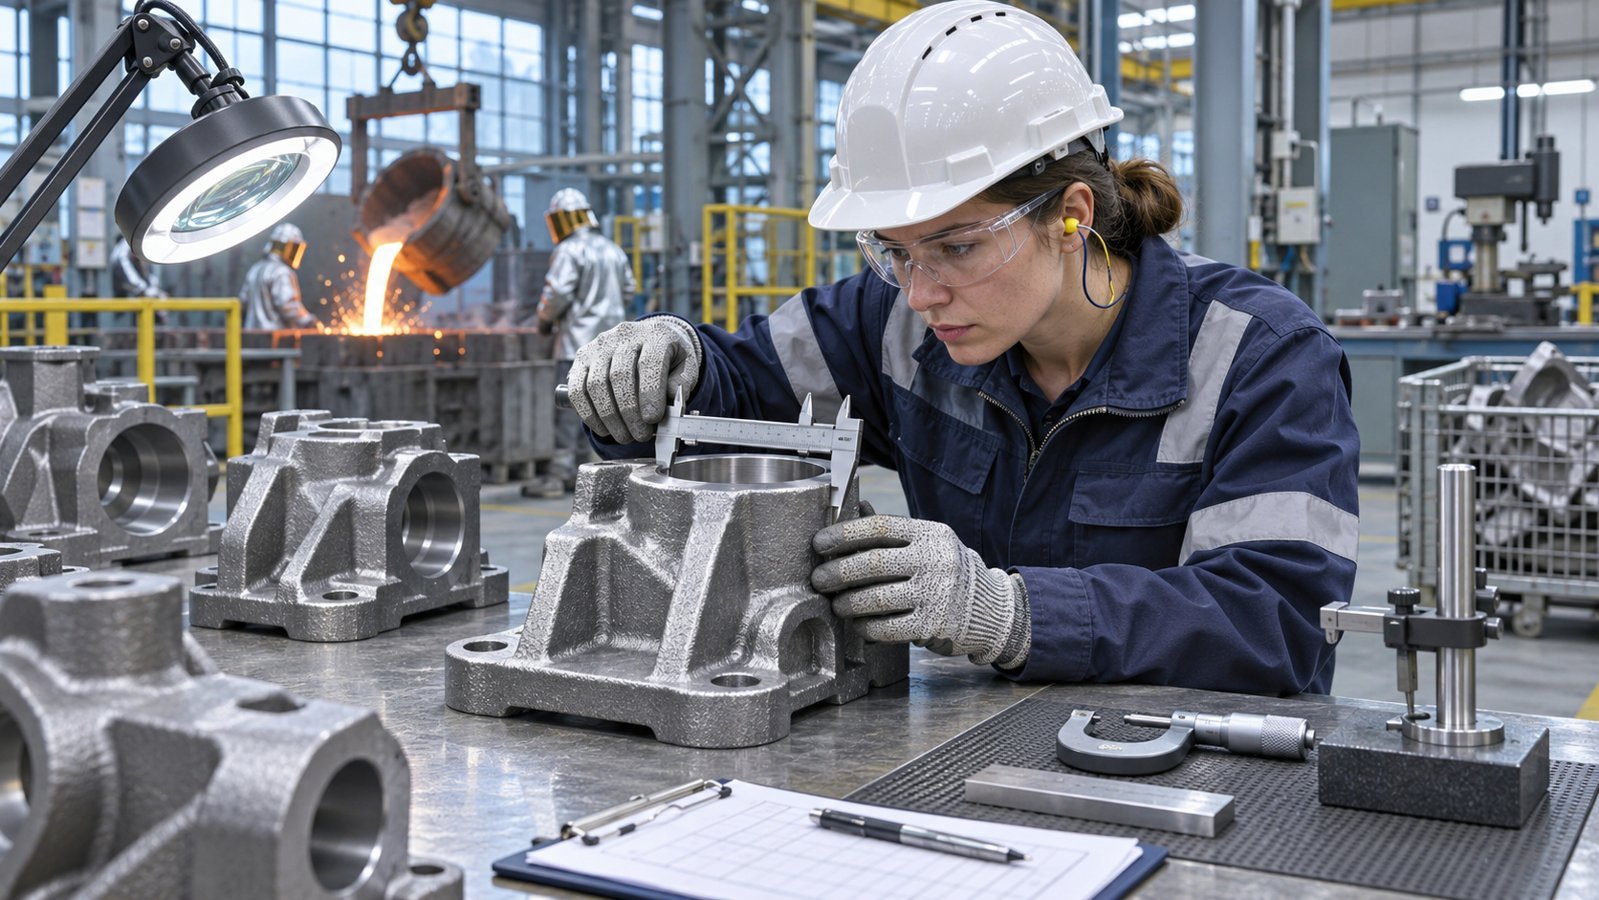
Foundry scrap tracking in ERP starts by recording what was rejected, where it was found and what happened next. Capture rework separately, then record its result. That gives production and quality teams a way to spot patterns without counting the same part as both recovered output and final scrap.
Which fields should the rejection record contain?
- Traceability: part and revision, work order, heat or lot, and affected quantity or weight.
- Observation: process stage, defect code and where the issue was detected.
- Disposition: hold, authorised rework, release or scrap, with approval and date.
- Financial follow-up: rework time and material, scrap recovery and any related cost references.
Keep defect and cause separate. For example, the inspector can record porosity at machining while the investigation establishes the underlying cause. That makes the first entry useful without turning an early theory into a permanent record.
Keep casting yield and unit scrap rate separate
The U.S. Department of Energy metalcasting study describes casting yield in terms of usable casting weight relative to poured metal. A unit scrap rate answers a different question. Specify the unit and the denominator in each report.
Example: Of 100 castings, 92 pass on the first inspection, six recover after approved rework and two are scrapped. First-pass acceptance is 92%, final accepted units are 98%, and final unit scrap is 2%. Track rework effort separately. You would still need weight data to calculate metal yield.
Build a weekly quality review
Group final scrap by part, heat or lot, process stage and defect. Review rework volume alongside it, so a lower scrap rate doesn’t hide a rising workload. Assign one person to close each investigation and record any corrective action against the original rejection.
See Velotech’s heat-to-shipment traceability guide and foundry ERP requirements checklist. Contact Velotech Solutions with a sample rejection record to discuss your ERP workflow.